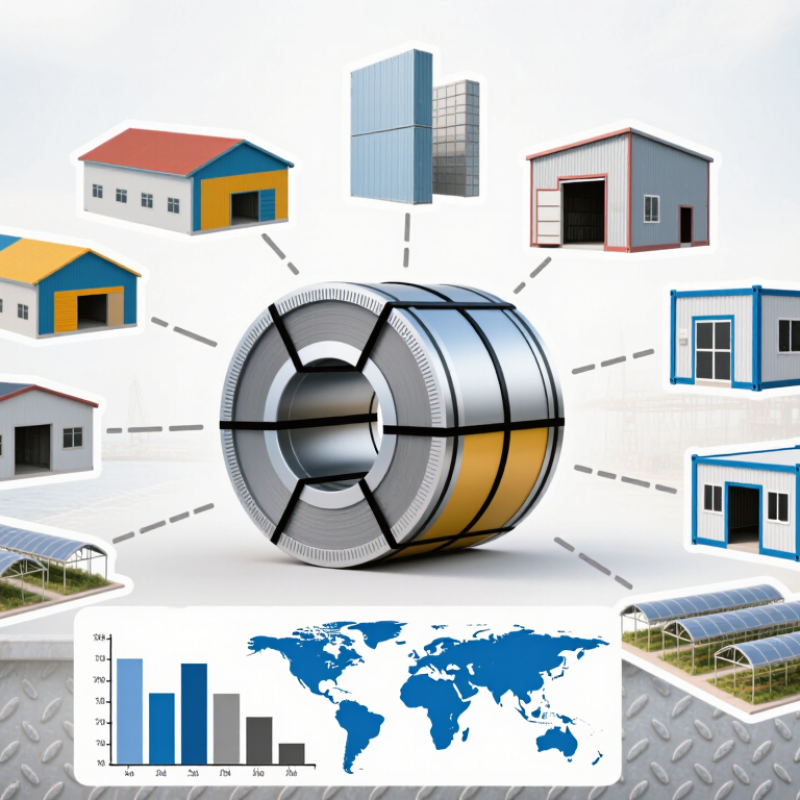
| 1. Steel Substrate Preparation | Low-carbon cold-rolled steel, commonly 0.20–1.20 mm thick and approximately 600–1,600 mm wide. | Provides the base strength, dimensional stability, and formability required for roofing, cladding, panels, and fabricated components. | Thickness, width, flatness, surface cleanliness, and mechanical properties are checked before coating. |
| 2. Continuous Hot-Dip Galvanizing | The cleaned steel strip passes through molten zinc at approximately 450°C; typical total zinc coating masses range from about 60–275 g/m² for both sides, subject to specification. | Zinc provides sacrificial corrosion protection and helps extend service life in many outdoor applications. | Coating mass, adhesion, surface appearance, and coating uniformity are verified across the strip width. |
| 3. Surface Treatment | Chemical pretreatment and, where specified, passivation or a thin protective film are applied before painting. | Improves paint adhesion, reduces storage staining, and supports consistent coating performance during forming and installation. | Treatment type must be compatible with the selected paint system, forming process, and environmental exposure. |
| 4. Primer Application | A corrosion-resistant primer is applied to the prepared steel, typically at a dry-film thickness of about 5–10 μm. | Creates an intermediate bonding layer and improves corrosion resistance beneath the topcoat. | Wet-film or dry-film thickness, coverage, adhesion, and curing conditions are controlled continuously. |
| 5. Organic Topcoat Application | A factory-applied organic coating is commonly around 15–35 μm on the exposed side; the reverse side may receive a thinner backing coat. | Provides color, gloss, weatherability, chemical resistance, and a uniform finish suitable for large-scale projects. | Color, gloss, coating thickness, flexibility, impact resistance, and adhesion are matched to the project specification. |
| 6. Curing and Cooling | The coated strip passes through an oven; the required peak metal temperature commonly falls within approximately 210–250°C, depending on the coating system. | Ensures the paint film develops the required hardness, adhesion, flexibility, and resistance to handling. | Oven temperature, strip speed, residence time, and peak metal temperature are recorded for process control. |
| 7. Quality Inspection | Typical checks include thickness, width, coating mass, color difference, gloss, pencil hardness, bend performance, impact resistance, and adhesion. | Reduces variation between production lots and supports reliable fabrication at different project locations. | Inspection criteria should be defined in the purchase specification and verified against applicable national or international standards. |
| 8. Slitting, Cutting, and Recoiling | The finished strip can be supplied in master coils, slit coils, or cut lengths according to the required dimensions and handling limits. | Enables efficient transport, localized processing, reduced site waste, and easier installation planning. | Edge condition, inner and outer diameter, coil weight, packaging, and marking are confirmed before dispatch. |
| 9. Global Project Suitability | Available in multiple substrate strengths, coating masses, paint systems, colors, widths, and thicknesses. | Supports standardized procurement for roofing, wall cladding, warehouses, agricultural buildings, modular structures, and general fabrication. | Final selection should consider climate, UV exposure, humidity, pollutants, forming method, design life, and local building requirements. |

 Your message must be between 20-3,000 characters!