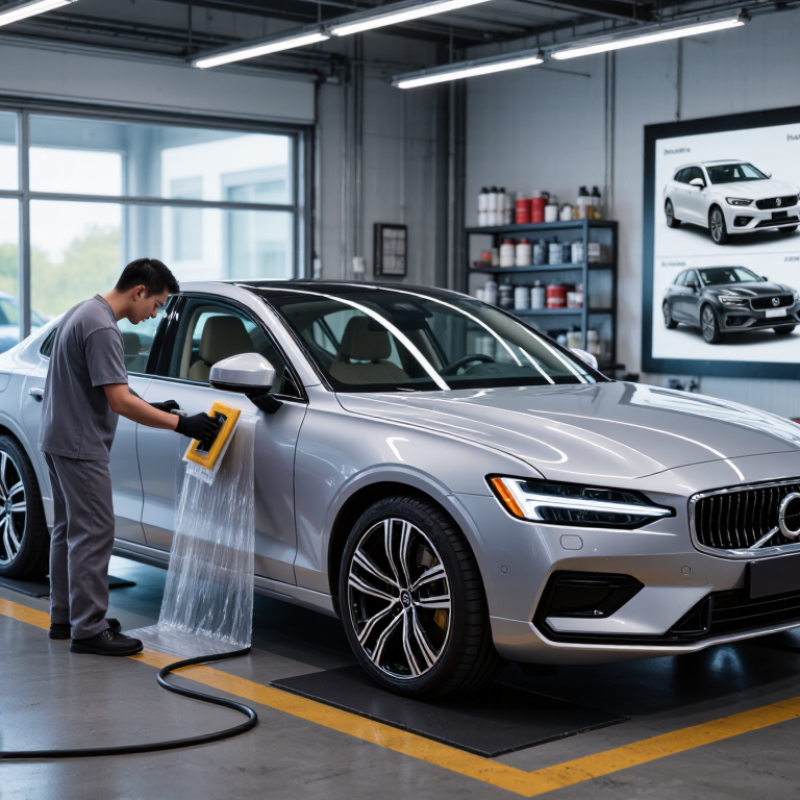
| 1 | Film Substrate Selection | Thermoplastic polyurethane (TPU) is commonly used as the main protective film substrate. Film formulations differ in flexibility, toughness, and resistance to environmental exposure. | Confirm polymer type and review the technical data sheet and material traceability records. | The substrate forms the film body and strongly influences flexibility, impact response, and long-term performance. |
| 2 | Substrate Forming | TPU may be produced as a continuous film using controlled film-forming and cooling processes. The precise production route depends on the material and equipment. | Check thickness consistency, surface defects, edge quality, and visible inclusions across the roll. | Consistent film formation helps prevent weak areas, uneven installation, and variations in appearance. |
| 3 | Thickness Control | Commercial paint protection films are commonly sold in thicknesses around 6–10 mil (approximately 150–250 µm); stated values may refer to different layer combinations. | Measure total thickness at multiple locations and confirm whether the stated figure includes coatings and adhesive. | Clear measurement definitions make product comparisons more meaningful and help assess installation characteristics. |
| 4 | Surface-Coating Application | A functional topcoat may be applied to improve cleanability and resistance to staining or surface marking. Some products are designed with heat-responsive surface recovery. | Inspect coating uniformity, gloss consistency, surface defects, and performance claims under stated test conditions. | The outer layer is exposed to road debris, cleaning chemicals, sunlight, and everyday contamination. |
| 5 | Adhesive and Release-Liner Lamination | A pressure-sensitive adhesive and a removable release liner are commonly combined with the film in a controlled lamination process. | Check for bubbles, wrinkles, contamination, liner release consistency, and adhesive transfer after removal. | Adhesive behavior affects positioning, installation, bonding, and eventual film removal. |
| 6 | Slitting and Roll Finishing | Finished material is slit to specified widths and wound into rolls under controlled handling conditions. | Inspect roll width, winding tension, telescoping, edge damage, and packaging protection. | Good roll finishing reduces handling damage and makes the film easier to process and install. |
| 7 | Optical Clarity and Haze | Clear-film appearance can be assessed using haze and light-transmission measurements; ASTM D1003 is a commonly referenced method for haze and luminous transmittance of transparent plastics. | Record test method, specimen preparation, haze, and light transmittance; also inspect for distortion and visible defects. | Optical quality affects the painted surface's appearance after the film is applied. |
| 8 | Adhesion and Peel Behavior | Peel adhesion can be evaluated using a defined substrate, application procedure, dwell time, peel angle, and test speed. ASTM D3330/D3330M is a reference method for peel adhesion of pressure-sensitive tape. | Report the complete test conditions and results rather than comparing peel values from different procedures. | Adhesion needs to balance secure bonding with practical installation and removal requirements. |
| 9 | Mechanical and Weathering Tests | Tensile properties may be measured using ASTM D882 for thin plastic sheeting. Accelerated UV and moisture exposure may use methods such as ASTM G154, with conditions selected for the product. | Document specimen preparation, exposure cycle, duration, and changes in appearance or measured properties. | Controlled tests help compare material behavior, but accelerated exposure does not directly establish a specific outdoor service life. |
| 10 | Final Quality Control and Traceability | Finished rolls can be sampled by production lot and checked against documented acceptance criteria before release. | Review inspection records, lot identification, packaging condition, retained samples, and corrective-action procedures. | Traceable records support consistent production and help identify the source of quality issues. |

 Your message must be between 20-3,000 characters!